



Induction Furnace or Crucible Furnace? Melting Non-Ferrous Metals Compared
Small and medium non-ferrous foundries often face the same decision: melt in a crucible furnace heated by gas or electricity, or in an induction furnace that generates heat in the metal itself? The answer depends on alloy range, batch sizes, melt quality and site infrastructure.
Induction Furnace vs Crucible Furnace: What Is the Difference?
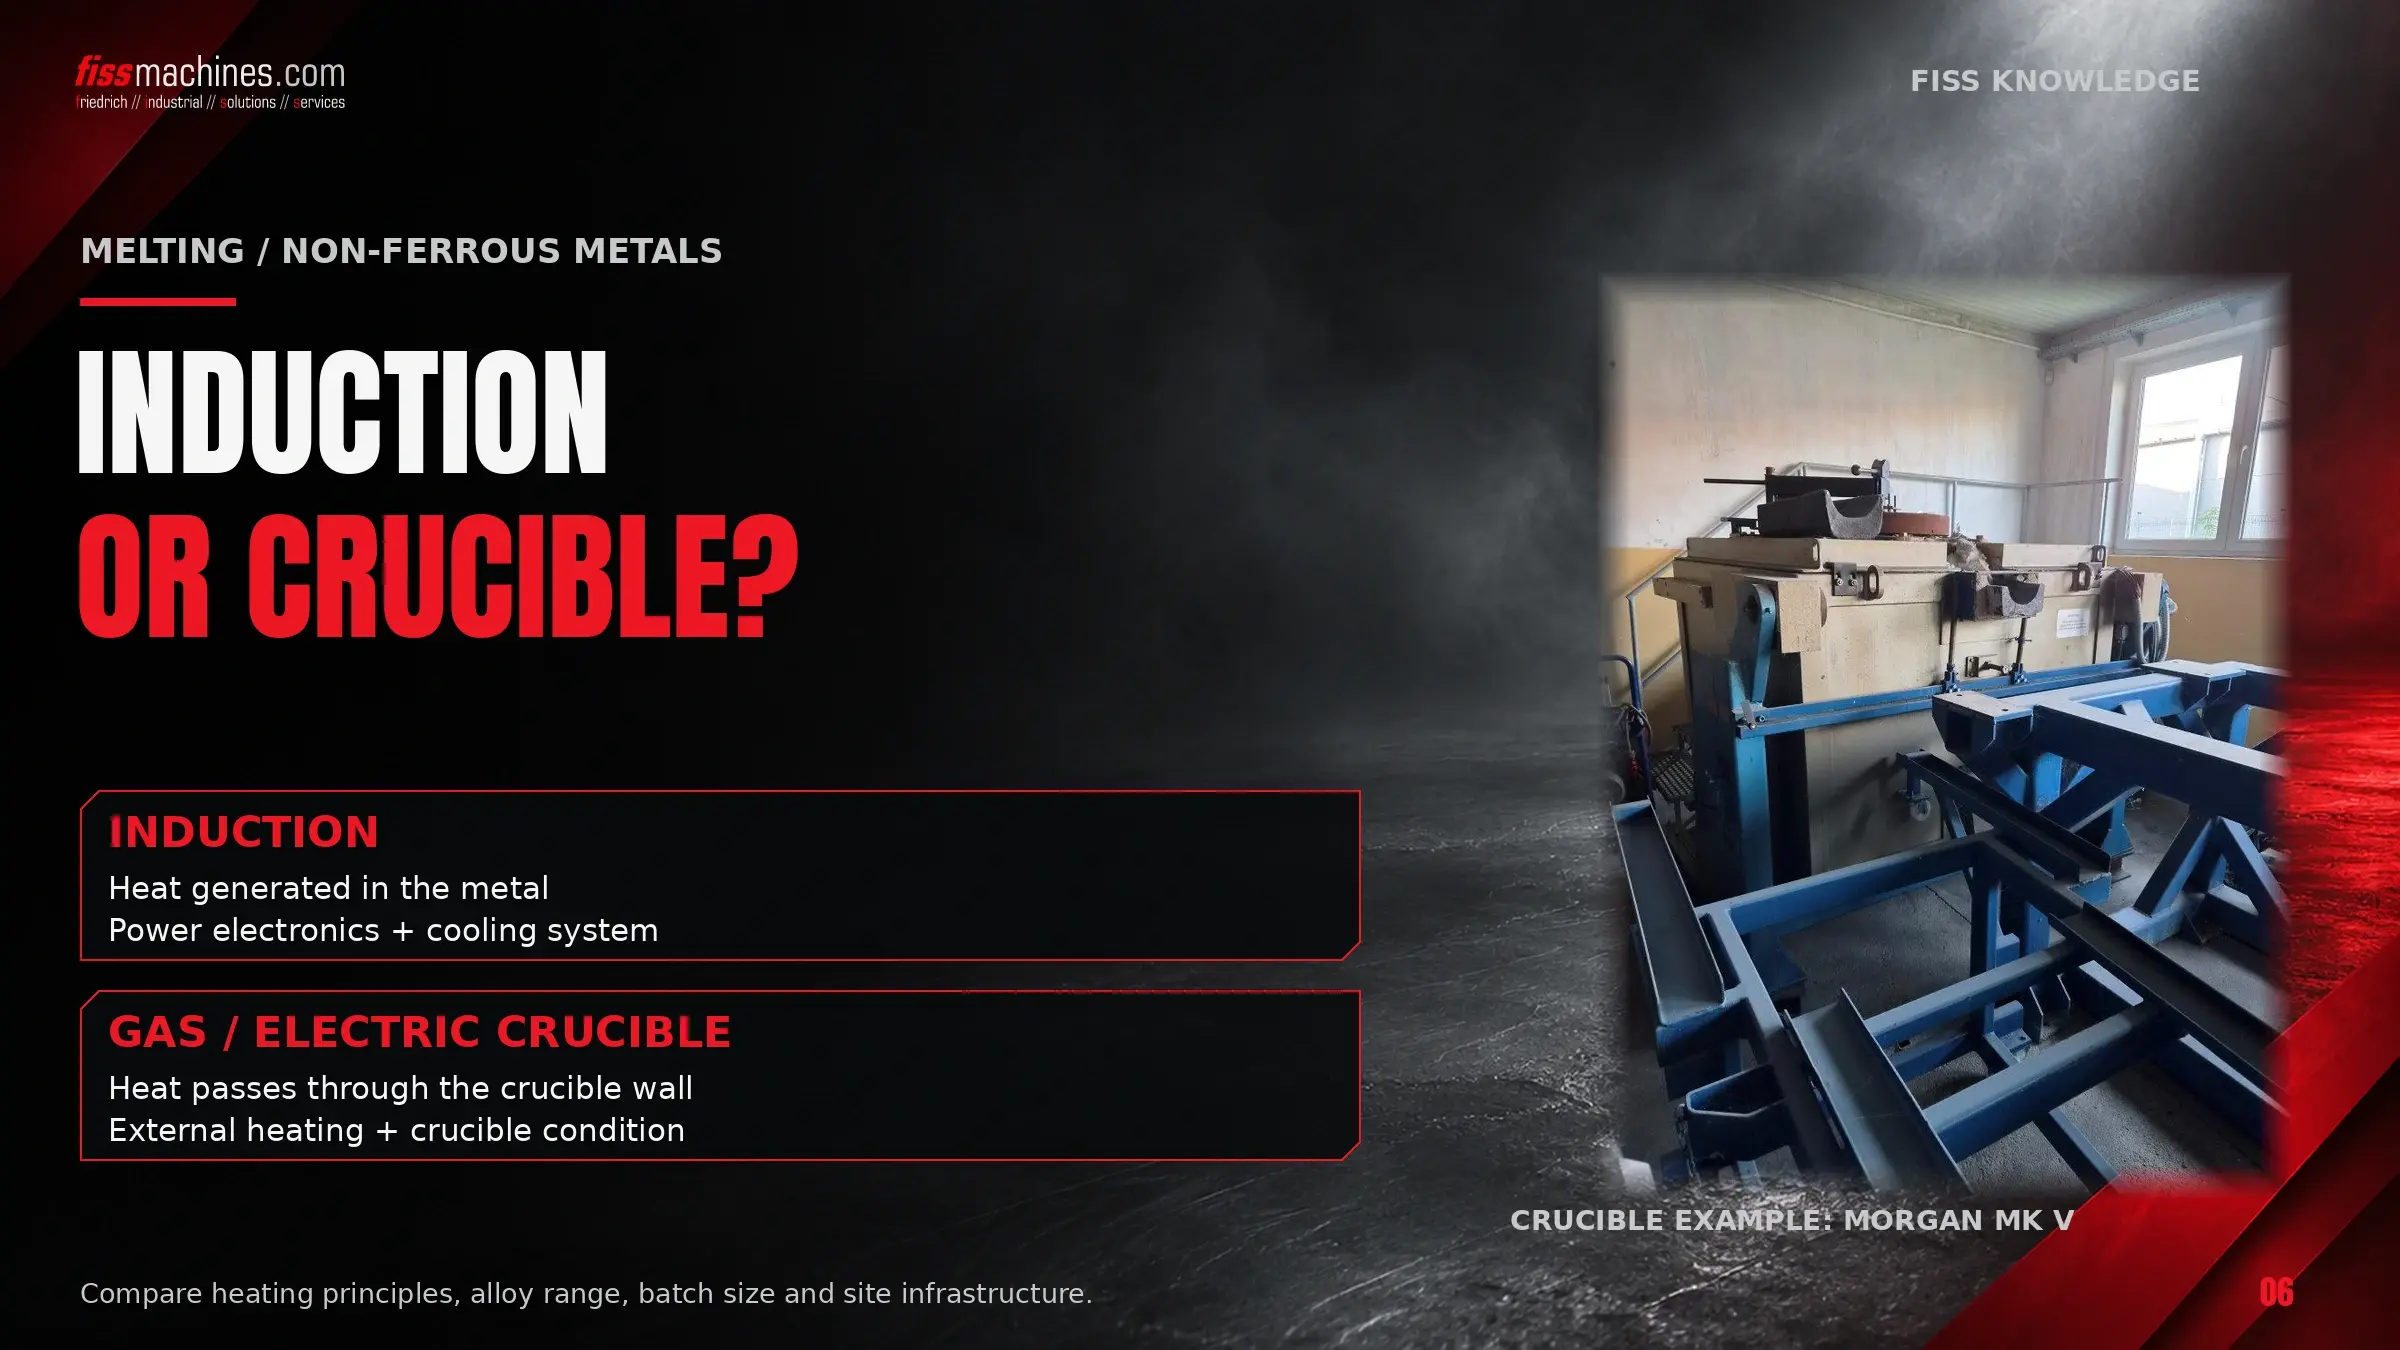
A crucible furnace heats a crucible from the outside – with a burner or with electric resistance elements – and the heat passes through the crucible wall into the metal. An induction furnace uses an alternating magnetic field from a water-cooled coil to generate the heat directly in the charge and moves the bath at the same time.
Crucible furnaces are simple, need little infrastructure and suit alloy changes in small lots. Induction furnaces melt faster and mix alloys well, but require a converter, cooling water system, strong power connection and strict safety discipline. For aluminium, the bath movement is both an advantage and a risk.
Three Ways to Get Heat into the Metal
This article compares heating principles. Which function a furnace has in the metal flow – melting, holding or dosing – is explained in Dosing Furnace, Melting Furnace or Holding Furnace?
Coreless Induction Furnace
A coil surrounds a refractory crucible or rammed lining. The field induces currents in the charge; heat is generated in the metal, and the bath is stirred electromagnetically.
Channel Induction Furnace
An inductor flanged to the furnace vessel heats metal in a closed channel loop. Mainly a holding and continuous-operation furnace.
Crucible Furnace
A burner or resistance elements heat a clay-graphite or silicon carbide crucible from outside. No electromagnetic stirring.
Coreless or Channel, Mains or Medium Frequency
The coreless induction furnace is the usual induction melting furnace for batch work. Otto Junker describes it as completely emptiable and “particularly suitable for flexible alloy changes and discontinuous batch operation”; the intensity of the bath movement can be influenced via the frequency. Modern units are powered by inverters using thyristor or IGBT technology.
The channel induction furnace works like a transformer whose secondary winding is the liquid metal in the channel. Otto Junker positions channel furnaces mainly as efficient holding units that decouple melting and casting; its subsidiary INDUGA builds channel melting furnaces for copper alloys and aluminium. For alloys prone to deposits, Otto Junker prefers crucible-type furnaces because of the risk of channel clogging.
Mains Frequency or Medium Frequency
Mains-frequency (50/60 Hz) furnaces were typically run with a liquid heel: according to Inductotherm, about 10–15 % of capacity stayed molten between taps, and turbulent low-frequency stirring required oversized furnaces. Solid-state medium-frequency inverters made batch melting practical – the furnace is emptied after each melt and can be shut down after the shift.
Stirring: Advantage for Alloying, Risk for Aluminium
Homogeneous Melt, Fast Alloying
Stirring distributes alloying elements and temperature. According to StrikoWestofen authors, it pulls chips below the surface – a precondition for low melting loss.
Oxides and Hydrogen
Excessive turbulence breaks the oxide skin of aluminium, folds oxide films into the melt and increases dross formation. Oxide formation and hydrogen pick-up are linked.
In practice, power and frequency are reduced once the charge is molten so that the bath surface stays calm. Degassing, filtration and oxide control are covered in Aluminium Melt Quality.
Gas or Electric, Tilting or Bale-Out
StrikoWestofen authors (2010) named the strengths of crucible furnaces: simple operation and maintenance, low investment and different alloys in small lots with quick changes. For larger volumes, they considered them uneconomical because of high specific energy use and manual operation.
Gas- or Oil-Fired
Nabertherm calls gas-fired furnaces ideal for melting. Excess air and flame impingement oxidise the crucible.
Electric Resistance
No combustion gases – one moisture source less for aluminium. Widely used for holding.
Tilting Furnace
The whole furnace tilts to pour into a ladle or mould, often with electro-hydraulic drive.
Bale-Out Furnace
Stationary furnace; metal is ladled out by hand or robot. Typical as holding furnace at the casting station.
Crucible Material and Wear
Common materials are clay graphite and silicon carbide (SiC). According to Foseco (Molten Metal Systems), the choice depends mainly on working temperatures and heating cycles. Typical causes of premature failure:
- Thermal shock from insufficient preheating after cooling
- Oxidation from excess air, flame impingement or long holding at low temperature
- Flux added with the solid charge instead of to the fully molten bath
- Dross build-up that expands and cracks the wall
- Heavy ingots dropped into the crucible, wedged charge material
Cracked crucibles should not be repaired but taken out of service immediately, as Molten Metal Systems recommends.
Side by Side for Typical Non-Ferrous Applications
| Criterion | Coreless Induction Furnace | Crucible Furnace (Gas / Electric) |
|---|---|---|
| Heat transfer | Generated directly in the charge | Through the crucible wall |
| Bath movement | Electromagnetic, adjustable via frequency and power | None; mixing by hand or rotor |
| Alloy change | Completely emptiable, suited to batches | Simple; dedicated crucible per alloy possible |
| Infrastructure | Converter, capacitors, cooling water system, high-power connection | Gas connection and exhaust, or electrical connection |
| Typical use | Copper alloys, aluminium with alloying, larger batches | Aluminium, zinc and copper alloys in small lots, holding at the casting station |
Cooling Water, Power Supply and Water–Melt Contact
An induction furnace is a system: coil, converter, transformer, capacitors, cooling, lining, control and power connection must work together. Coils, inverters and cables are water-cooled.
The greatest hazard is water meeting molten metal: it turns to steam instantly and can cause an explosion. Inductotherm engineers warn that a run-out through a failed lining can damage the coil, letting cooling water reach the metal. Wet or sealed charge is dangerous in both furnace types.
- Check the refractory lining before every melt (AFS: fins, flaking, erosion, build-up)
- Test the ground leak detector as specified by the manufacturer
- Check water levels and leaks – leaks cause coil arcing
- Charge only dry, preheated material
- Crucible furnaces: emergency outlet and collecting pan for crucible breakage
Energy Figures: Only with Context
Comparisons only make sense for the same alloy, temperature, batch size and operating mode. Published values are mostly manufacturer statements: StrikoWestofen authors gave approx. 130–150 m³ of gas (cold-air burners) or around 400 kWh of electricity to melt one tonne of aluminium to 720 °C in crucible furnaces. Otto Junker states 7–9 % savings from a multi-layer coil for copper and aluminium alloys. Holding times, lids and returns often matter more – see Energy Efficiency in Die Casting.
What to Check on a Used Furnace
Coil, Converter, Cooling
Coil and water leaks, lining, converter generation (thyristor or IGBT) and spare parts, capacitors, cooling circuit, ground leak detector, documents.
Heating, Insulation, Mechanics
Burner or elements, insulation and shell hot spots, tilting hydraulics, emergency outlet, availability of replacement crucibles.
Check the power connection and cooling water capacity at the new site before buying an induction furnace. FISS lists used furnaces – including induction and crucible furnaces – in its furnace overview; availability changes with stock.
The Process Decides, Not the Furnace Type
Crucible furnaces remain the pragmatic choice for many alloys in small lots with little infrastructure. Induction furnaces are stronger where fast melting, alloying and returns count – provided power, cooling water, safety and careful bath control for aluminium are in place.
Questions About Induction and Crucible Furnaces
Can Aluminium Be Melted in an Induction Furnace?
Yes. Coreless induction furnaces are used for aluminium, especially for returns and chips. To limit oxide and hydrogen pick-up, the bath movement is reduced after melting and the melt is treated before casting.
Why Are Channel Furnaces Rarely Used for Alloy Changes?
The channel must stay filled with liquid metal, so channel furnaces run continuously. Coreless induction and crucible furnaces can be emptied completely.
How Long Does a Crucible Last?
There is no general figure. Service life depends on alloy, temperature, flux, charging and preheating. A use log helps to plan replacement but does not replace inspection.
Gas or Electric Crucible Furnace?
Gas-fired furnaces are strong in melting; electric furnaces avoid combustion gases and are widely used for holding. Local energy prices, available connections and emission requirements usually decide.
Used Crucible and Induction Furnaces from FISS.
FISS lists used crucible furnaces, induction furnaces and melting furnaces for non-ferrous foundries and helps clarify which design fits your alloys, batch sizes and site.
Sources
Otto Junker: Medium-frequency coreless induction furnace and Channel-type holding furnace, otto-junker.com, accessed 5 November 2026.
K. Malpohl, R. Hillen (StrikoWestofen): Aluminium melting furnaces for die casting, Foundry-Planet, 2010.
S. Prabhu (Inductotherm): More Powerful Induction Furnaces and Inverters, Foundry Management & Technology, 2011.
E. Tabatabaei, R. C. Turner (Inductotherm): Molten Metal Splash and Furnace Refractory Safety, Foundry Management & Technology, 2009.
AFS Institute: Back to Basics: Induction Furnace Daily Maintenance, Modern Casting, 2023.
Foseco / Molten Metal Systems: Frequently Asked Questions about Crucibles, foseco.com, accessed 5 November 2026; Foundry Management & Technology: Top 10 Ways to Maximize Crucible Service Life, 2013.
Nabertherm: tilting furnaces K, KB, KBR and bale-out furnaces T for melting and holding, nabertherm.com, accessed 5 November 2026.
ICSOBA 2023: Initiatives to Minimize Dross Generation in Casthouse (paper CH04).
